How to Choose a Vibration Solution for an Industrial Site
Most bad vibration jobs begin with the wrong sequence rather than the wrong isolator. Lock in machine speed, weight, mounting point and support stiffness first, and the right choice is mostly maths.
Start with machine data, not the catalog
Every isolation decision flows from forcing frequency, which is the excitation your machine puts into the structure. You can get it directly from operating speed. Divide RPM by 60 to get Hz. A 1750 RPM motor excites at about 29 Hz, while a 1450 RPM motor sits near 24 Hz and a 900 RPM fan sits at 15 Hz.
You also need the true operating weight and weight split. Nameplate weight is not enough when a pump is wet and piped. Find the centre of gravity and the load at each mount. Uneven loading is common on packaged skids where the motor hangs off one end. If you size four identical mounts for the average load, the lightly loaded corner will not deflect enough, so its natural frequency will not match the rest.
Mounting location can change the problem as much as the machine. A thick ground slab on compacted fill is stiff and forgiving. An elevated slab or steel mezzanine is flexible and has its own resonance to consider. Reciprocating machines and crushers deliver low-frequency, high-amplitude force that needs soft support. High-speed rotary machines buzz at a higher frequency with lower amplitude, calling for a different answer. Write this information down before you open a catalogue and you will avoid most construction rework caused by the wrong mounts arriving after the slab is poured.
Run the frequency ratio test
An isolator has its own natural frequency. Think of it as the bounce rate of the spring and mass together. When the machine’s forcing frequency is close to that bounce rate, vibration is amplified. When the forcing frequency is well above it, vibration is reduced. Transmissibility expresses this relationship. A value below 1.0 means less force reaches the structure than the machine produces.
Isolation does not start until the forcing frequency exceeds the natural frequency by a factor of the square root of two, or about 1.414 times. In practice, we do not aim for the edge of that curve. A forcing frequency at least three times the isolator’s natural frequency is a more useful target. That frequency ratio of 3 to 1 delivers roughly 85 to 90 percent isolation on paper. A 29 Hz machine therefore wants an isolator natural frequency near 9 Hz or lower. A 15 Hz machine wants 5 Hz or lower, which requires a much softer mount.
Low-speed machines are harder to isolate. There is a firm limit here. You cannot isolate a 7 Hz excitation with a pad whose natural frequency is 11 Hz because it will amplify the vibration. This single check rules out many bad specifications. If a supplier cannot tell you the natural frequency at your load and the resulting transmissibility, you do not have a finished specification yet. You have a guess.
On a construction project with mixed plant, this test sorts equipment quickly. Small high-speed pumps will pass with simple pads, while large slow fans will not. That is physics rather than a brand difference. Once the team sees the maths, there is usually less argument about cost.
Use static deflection as your field shortcut
Natural frequency may sound like a laboratory measure, but there is a practical site shortcut. For steel springs and rubber mounts, natural frequency tracks static deflection. The handbook relation is natural frequency in Hz equals 15.8 divided by the square root of deflection in mm under actual load. A 25 mm deflection gives about 3.2 Hz. A 50 mm deflection drops that figure to about 2.2 Hz.
A 6 mm deflection sits near 6.5 Hz, while a 2 mm pad sits near 11 Hz. Those numbers explain why thin elastomeric pads only suit fast machines. If your forcing frequency is 29 Hz and the pad’s natural frequency is 11 Hz, the ratio is about 2.6 to 1, so you will get some isolation. If the forcing frequency is 15 Hz with that same pad, the ratio is near 1.4 to 1. You will get no useful isolation and will sit right on the amplification hump.
You can check deflection with a tape and a load. Measure the free height, then the fitted height under full wet weight with the pipes filled. The difference is the real deflection. Compare it with the catalogue curve at that load, not at maximum load. If the numbers do not line up, trust the site measurement. Pads that have taken a set or springs that are coil-bound will not follow the brochure.
During construction handover, this check takes minutes and can settle arguments. We have seen pads specified for 6 mm that deflect only 3 mm because the machine is lighter than planned. That pushes the natural frequency up and wipes out the predicted performance.
Match isolator media to the duty
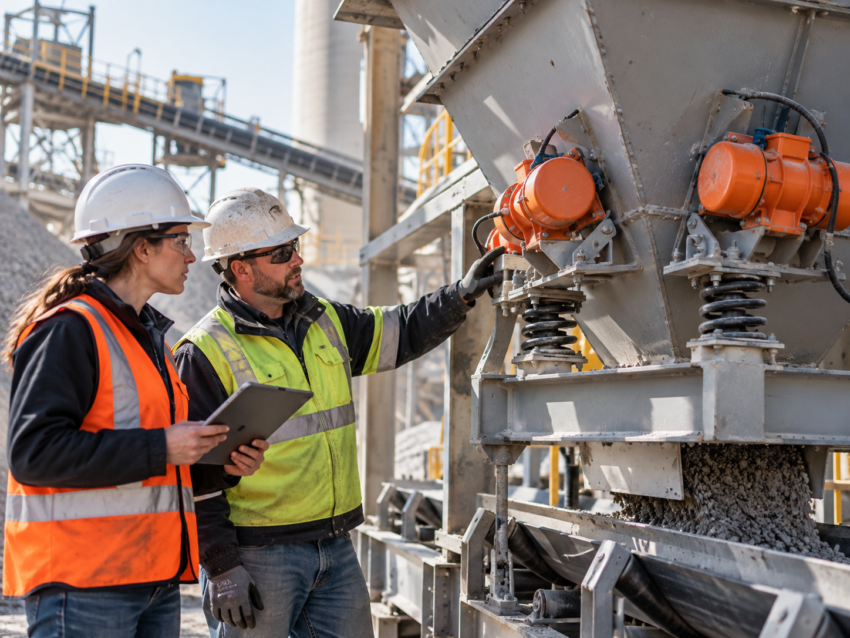
Helical steel springs handle low-frequency, high-amplitude work. They can be built for 25 mm to 75 mm deflection without becoming unstable. That makes them the default for crushers, screens, large fans and reciprocating compressors that run slowly and punch hard. They tolerate substantial movement while keeping the natural frequency low on machines running below 1200 RPM. On bulk-material handling lines, some vibration is intentional rather than a fault to eliminate. Purpose-built vibration solutions can help prevent bridging and maintain material flow through hoppers and chutes; isolation mounts perform the separate job of limiting vibration transmitted into the structure.
Elastomeric mounts made from neoprene or natural rubber suit the other end of the range. They provide 2 mm to 8 mm deflection and add damping that controls high-frequency buzz. Use them on small inline pumps, high-speed fans, packaged units and fan coil modules running above 1500 to 2000 RPM, where the required frequency ratio is easier to achieve. They are simple, and they resist corrosion in damp plant rooms.
Trouble starts when the two are swapped. Rubber pads under a slow crusher will amplify force into the slab. Soft springs under a high-speed, lightweight pump can transmit more structure-borne noise through the spring coil than a rubber pad would. Springs isolate force well, but steel carries high-frequency noise along the coil unless the mount includes rubber cups or pads. Pick the medium for frequency and amplitude first, then address noise with acoustic breaks where needed.
Check ratings at your actual load
Catalogue ratings can mislead when you read the wrong column. A mount rated to 1000 kg may show 15 mm deflection at that maximum. Put only 400 kg on it and the deflection may drop to 5 mm. Natural frequency then climbs from about 4 Hz to about 7 Hz. Your predicted 85 percent isolation can fall to near zero without anything appearing visibly wrong.
Catalogue maximums often mislead more than they help.
Always ask for load versus deflection and transmissibility curves instead of relying on a single maximum number. You need the curve point at the actual corner load, with wet weight and attached services included.
Good data sheets show deflection and transmissibility at several loads across the operating range. Compare two or four competing mounts at your load rather than at their maximum. Look for actual load performance in writing and keep that sheet in your commissioning file.
If corner loads vary by more than 15 percent, split the schedule. Use different mounts from front to rear or add ballast to balance the frame. It costs less than rework after the screed is down and the pipework is hung.
Design for location and connections
Where the machine sits determines how soft the support must be. A 200 mm ground slab spreads force and forgives small errors. A rooftop frame or steel mezzanine flexes with the machine and may resonate near the forcing frequency. On flexible supports, point isolator maths alone will not solve the problem because rocking modes appear that a single-degree calculation misses.
This is where inertia bases earn their keep. A concrete inertia base bolts to the machine, with the isolators positioned under the base. The added mass lowers the combined natural frequency and steadies top-heavy pumps and tall fans that tend to rock. On elevated steel or lightweight mezzanines, a base with springs is often the only combination that achieves the ratio while keeping movement stable.
Flanking paths can quickly undo good mounts. A pump on correctly selected springs will still shake the building if its discharge pipe is hard-connected to the wall. Treat pipes, ducts, conduit and cable tray as parts of the isolation system. Use flexible couplings close to the machine, rubber spool pieces on pump connections, and braided drops with flexible conduit on electrical feeds. Hang the first few pipe supports on isolation hangers so vibration does not re-enter the slab nearby.
Bring this work into the construction programme early. Slab thickness, housekeeping pads, foundation depth and anchor layout are set during the build. Specifying isolators after the pour or after cables are pulled leaves constraints that force compromises. Retrofitting a live plant costs far more in cutting, coring, lifting and downtime than setting the plinth height and bolt positions correctly during new construction.
Plan for startup and site conditions
Rotating machines cross resonance during every start and stop. As speed ramps up, the forcing frequency sweeps past the isolator’s natural frequency. Amplitude briefly spikes even in a well-designed system. For most fixed-speed plant, that spike is short and harmless. For tall mounts, soft springs, seismic zones and outdoor frames, add snubbers or restraints that limit travel without shorting the mount.
Environmental conditions often damage mounts faster than load. Oil softens natural rubber and swells cheap pads. Ozone, UV, washdown chemicals and process fumes crack exposed elastomers over time. Specify oil-resistant neoprene where oil is present. Use coated springs with drainage and covers in outdoor or corrosive areas.
Close out the job with a loaded check. Run the plant at full operating temperature and load, then measure vibration velocity at the bearings and feet. Compare the readings with ISO 10816 zone limits for acceptance. That standard will not design the mounts, but it provides a clear pass or investigate line that both contractor and client can understand. Re-torque the isolator bolts and check deflection again after the first week, once pads have taken a set and springs have settled.
File the as-built loads, measured deflections, velocity readings and photos with the maintenance manual so the next change-out reflects site reality rather than the tender estimate. That record keeps the next motor swap from restarting the entire problem.
Pick mounts from machine data and prove the ratio before purchase. Detail bases, pipe breaks, restraints and hanger locations in the same package. Sites that follow that sequence get quieter floors and fewer call-backs.